If you’ve ever walked the floor of a job shop making aerospace components, medical implants, or heavy industrial gear, you know the difference between a machining center that gets you through the day and one that makes you look forward to every shift. I’ve been selling horizontal machining centers (HMCs) for 18 years, and I’ve seen a lot of machines come and go. The ones that stand the test of time, that customers call “game changers” a year after installation, all share a set of non-negotiable features. These aren’t flashy add-ons or marketing buzzwords—they’re engineering choices that directly translate to fewer downtime hours, tighter tolerances, lower per-part costs, and the ability to take on jobs you once thought were too complex to bid on. Horizontal Machining Center

Let’s start with the core structural foundation, because a machining center is only as good as its base. You wouldn’t build a skyscraper on sand, and you don’t build a high-end HMC on a thin, cast iron frame stamped from low-grade iron. I’ve had customers tell me they saved 20% on a competing HMC that cracked its spindle housing after six months of running uninterrupted 24/7 on titanium. The right structural design starts with a heavy, rigid cast iron base that’s been stress-relieved twice: once right after casting to release residual stresses, and again after machining critical surfaces. This isn’t just about durability—it’s about thermal stability. High-volume, tight-tolerance jobs generate a lot of heat, whether from the spindle cutting through hard materials or the motor driving the axes. A well-designed HMC will also feature a symmetric frame design, so heat is distributed evenly across all axes, not just focused on one side. I remember a customer in Michigan who was running 1,000 6061 aluminum parts a week on an older vertical machining center (VMC) before upgrading to our HMC. Their part dimensional variation went from +/-0.002 inches with the VMC to +/-0.0005 inches with the HMC, and half the scrap rate they were dealing with came from heat-induced deflection. That’s the base doing its job.
Next, the spindle—this is the heart of any HMC, and high-end models don’t cut corners here. Let’s talk about two key spindle features: speed and torque, but more importantly, the ability to balance both, plus the spindle’s runout tolerance. A lot of entry-level HMCs come with a 10,000 RPM spindle that’s under-torqued for heavy cuts, or a high-torque spindle that can’t reach above 6,000 RPM, making it slow to cut aluminum or composites. High-end HMC spindles are designed with power density in mind: typically 15 to 30 horsepower, with the ability to maintain consistent torque across a wide RPM range. For example, a 25 horsepower spindle might put out 100 foot-pounds of torque at 500 RPM and still hit 15,000 RPM for light finishing passes, no drop in power. Even more critical is TIR (total indicator runout), which measures how much the spindle wiggles when it spins. A bad TIR will ruin precision parts, especially those with small features or tight fits. High-end HMC spindles have a TIR of less than 0.0001 inches at the gage line—about a tenth the thickness of a human hair. I’ve got a medical device customer who runs bone plates, and their requirement is 0.0002 inch TIR max; a lower-end HMC would hit that on a good day, but our HMC holds it consistently, so they don’t have to rework every third part.
Then there’s the workholding and pallet system, which is where horizontal machining really shines over vertical. Waiters and waitresses can tell you about multitasking—your HMC should do the same. The horizontal orientation lets you machine all sides of a part in one setup, but only if you have a reliable way to hold the part, load it, and switch between jobs without losing position. High-end HMCs use full tombstone systems or modular workholding that’s hardened and precision-ground, so you can swap a tombstone without having to re-calibrate it every time. Pallet changers are another big one: entry-level HMCs might have a manual pallet change, which means your operator is waiting around while parts are loaded and unloaded, not running the next job. High-end models offer automatic pallet changers (APCs) with 2, 4, or even 8 pallets, so you can be machining one part while the next one is being prepped on the pallet off to the side. Some of our customers run lights-out operations three nights a week, and that’s only possible because the pallet system is fast—changeover in 90 seconds or less—and repeatable, so every pallet locks into the exact same position, time after time. I had a customer making hydraulic manifolds who used to spend two hours a day loading parts into a VMC; with our HMC’s 4-pallet APC, that time dropped to 15 minutes, and they can run 20% more parts a week now. The workholding also needs to be customizable: if you’re running large, heavy parts like engine blocks or aerospace bulkheads, the system should handle 1,000 pounds or more, without deflecting. Entry-level workholding uses thin, soft jaws that can bend under load, leading to part variation; high-end systems use hardened steel jaws or hydraulic workholding that applies consistent clamping force across the entire part, so even the heaviest cuts don’t shift the workpiece.
Tool changers are another make-or-break feature. If your HMC runs out of tools mid-job, you’re looking at hours of downtime—time you can never get back. High-end HMCs have large tool magazines, usually 30 tools minimum, and often up to 120 or more for jobs that require multiple operations. But size isn’t everything: the tool changer’s speed and reliability matter too. A fast tool change time reduces cycle time, and a reliable tool changer means no more jams or broken tool pull studs. I’ve seen cheap tool changers that take 10 seconds to swap a tool and jam twice a week; our high-end HMCs change tools in 2.5 seconds on average, and we’ve had less than one jam per 1,000 hours of operation in the field. Another key feature is tool life management. High-end HMCs come with built-in software that monitors tool wear, tracks how many parts each tool has cut, and alerts the operator when a tool is due for replacement before it breaks, mid-cut. For hard materials like Inconel or titanium, this is a lifesaver—replacing a $50 tool mid-job can ruin a $5,000 part, so catching wear early is non-negotiable. Some models even have automatic tool measurement, so you don’t have to manually calibrate each tool’s length and diameter, which saves time and eliminates human error.
Thermal management is a feature that most customers don’t think about until they’re having problems with part variation, but it’s one of the biggest differences between high-end and mid-range HMCs. Earlier, I mentioned thermal stability of the frame, but it doesn’t stop there. High-end HMCs use cooling systems for the spindle, the ballscrews, and even the axis motors, so their temperature stays consistent, regardless of how long the machine has been running. Mid-range models might cool the spindle, but not the ballscrews, which expand as they heat up, leading to axis positioning errors. I had a customer in the energy sector who was running 20-hour production runs on valve bodies, and their mid-range HMC’s X-axis would drift 0.003 inches over the course of a shift, leading to 10% scrap. After switching to our HMC, which has ballscrew cooling, that drift dropped to less than 0.0005 inches over the same run length—no more scrap, no more adjusting the machine every morning. Some high-end models even have a thermal compensation software module that automatically adjusts axis positions based on real-time temperature readings, so even if there’s a minor fluctuation, the machine corrects for it without operator input. That’s the kind of feature that doesn’t show up in the spec sheet, but it’s the reason a customer can run a 100-part batch with zero variation, no matter how hot it is in the shop floor.
Finally, control and connectivity. A high-end HMC isn’t just a machine—it’s part of your smart factory. The control system should be user-friendly enough for an experienced operator to learn in a day or two, but powerful enough for advanced programming, like 5-axis simultaneous machining or high-speed cutting. The latest controls have built-in diagnostic tools that can alert technicians to a potential problem before it causes downtime—like a loose belt or a filter that’s nearing the end of its life, so you can schedule maintenance during a lull, not in the middle of a rush job. Connectivity is also key: modern HMCs should integrate with your company’s ERP and MES systems, so you can pull job orders, track part production in real time, and monitor machine uptime remotely. I have a customer with three of our HMCs, and they can check each machine’s current status from their office, see how many parts it’s run that day, and even adjust a job schedule remotely without stepping foot on the shop floor. That level of integration isn’t possible with older, lower-end machines, which are isolated from the rest of the production workflow.
Now, let’s be clear: a high-end HMC isn’t cheap. But when you add up the costs—scrap parts, downtime, operator time, overtime, and missed jobs because your old machine can’t handle complex work—the return on investment is almost always within 18 to 24 months. I’ve had customers come to me after running a VMC for 10 years, saying they thought upgrading to an HMC was out of their budget, but after switching, they’ve been able to take on three new contracts that they would have lost to competitors with HMCs. The features I’ve talked about—rigid stress-relieved frame, precision spindle, reliable pallet and tool systems, thermal management, smart controls—aren’t just bells and whistles. They’re the difference between a machine that works for you and a machine that you work for.
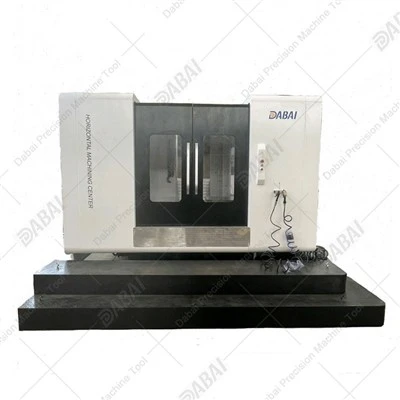
If you’re tired of scrap parts that cut into your profits, downtime that pushes back delivery dates, or jobs you can’t quote because your machine isn’t precise enough, it’s time to talk. We work with job shops, aerospace companies, medical manufacturers, and industrial plants of all sizes, and we’ll help you find the right HMC for your specific needs, not just a one-size-fits-all model. We don’t sell machines that look good on a trade show floor—we sell machines that run for years, that adapt to your growing business, and that give you a competitive edge. Reach out to start the conversation about your production goals, and let’s find the solution that will make your shop more efficient and profitable.
Vertical Machining Center References
- Flint, E. (2022). Machining Center Technology: A Guide to Rigidity, Accuracy, and Productivity. Industrial Press Inc.
- Koenigsberger, F., & Tlusty, J. (2019). Machine Tool Structures: Vibration, Rigidity, and Thermal Effects. Springer.
- American Machine Tool Distributors’ Association. (2021). Horizontal Machining Center Performance Metrics and Best Practices. AMTDA Technical Report.
- Shaw, M. C. (2018). Metal Cutting Principles. Oxford University Press.
Dabai Precision Machine Tool (Jiangsu) Co., Ltd.
As one of the most professional horizontal machining center manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy advanced horizontal machining center for sale here from our factory. We also accept customized orders.
Address: No. 66-1, Zhenhu North Road, Hudai Town, Binhu District, Wuxi City
E-mail: elaine@dabaicnc.com
WebSite: https://www.cnc-dabai.com/
